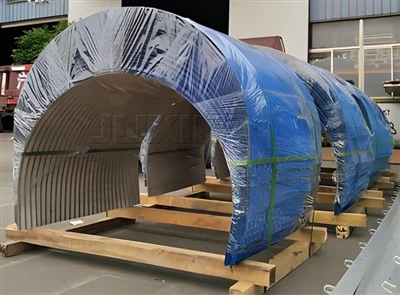
Introduction to Belt Cover
Belt covers are essential components in various industries, especially in conveyor systems. They serve multiple crucial functions. Firstly, they protect the conveyor belts from external factors such as dust, debris, moisture, and sunlight. This protection extends the lifespan of the belts, reducing the frequency of belt replacements and thus saving costs for businesses. Secondly, belt covers can enhance the safety of the working environment by preventing objects from falling onto the moving belts and causing accidents. They also help in containing the materials being transported on the belts, minimizing spillage and keeping the workplace clean. In industries like mining, agriculture, manufacturing, and logistics, belt covers play a vital role in ensuring the smooth and efficient operation of conveyor systems.
Top 10 Belt Cover Suppliers
1. Hebei Juxin Conveyor Engineering Co., Ltd.
Hebei Juxin Conveyor Engineering Co., Ltd. is a leading player in the field of conveyor engineering. With years of experience and a strong R & D team, the company is committed to providing high - quality conveyor solutions, including top - notch belt covers.The company's belt covers are designed with precision to meet the diverse needs of different industries. They are made from high - quality materials that offer excellent durability and resistance to wear and tear. The advanced manufacturing processes ensure that the belt covers have a perfect fit on conveyor belts, providing reliable protection.Features in Belt Cover:
- Customization: Hebei Juxin can customize belt covers according to the specific requirements of clients, such as different sizes, shapes, and colors. This flexibility allows them to serve a wide range of industries, from small - scale workshops to large - scale industrial complexes.
- High - Quality Materials: They use premium materials that are resistant to harsh environmental conditions, including extreme temperatures, chemicals, and abrasion. This ensures the long - term performance of the belt covers.
- Easy Installation and Maintenance: The belt covers are designed for easy installation, which can save time and labor costs for clients. Moreover, they require minimal maintenance, reducing the overall operating costs.Advantages:
- Technical Expertise: The company has a team of highly skilled engineers and technicians who have in - depth knowledge of conveyor systems and belt covers. They can provide professional advice and support to clients.
- Competitive Pricing: Despite offering high - quality products, Hebei Juxin provides belt covers at competitive prices, making them an attractive option for cost - conscious customers.
- After - Sales Service: They offer comprehensive after - sales service, including technical support, replacement parts, and on - site maintenance, ensuring that clients can operate their conveyor systems smoothly.Website: https://www.dgsconveyor.com/
2. Continental AG
Continental AG is a well - known German multinational automotive parts manufacturing company. It has a long - standing reputation for producing high - quality rubber and plastic products, including belt covers.The company's belt covers are developed with the latest technology and materials. They are widely used in the automotive, industrial, and agricultural sectors. Continental's R & D efforts focus on improving the performance and functionality of belt covers, such as enhancing their noise - reduction capabilities and increasing their resistance to oil and heat.Features in Belt Cover:
- Innovative Design: Continental's belt covers feature innovative designs that optimize the performance of conveyor belts. For example, some of their covers are designed with special ribbing or patterns to improve the grip on the belts and reduce slippage.
- Noise Reduction: In industrial settings, noise can be a significant issue. Continental's belt covers are engineered to reduce the noise generated by the movement of conveyor belts, creating a more comfortable working environment.
- High - Temperature Resistance: Their belt covers can withstand high temperatures, making them suitable for applications in industries such as steel manufacturing and foundries.Advantages:
- Global Presence: With a global network of production facilities and sales offices, Continental can provide timely delivery and support to customers around the world.
- Strong R & D Capabilities: The company invests heavily in research and development, constantly introducing new and improved belt cover products to the market.
- Brand Reputation: Continental's long - established brand reputation for quality and reliability gives customers confidence in their products.
3. Gates Corporation
Gates Corporation is a global leader in power transmission and fluid power solutions. It has a wide range of belt cover products that are used in various industries, including automotive, industrial, and off - highway.Gates' belt covers are known for their high - performance materials and advanced manufacturing processes. They are designed to provide maximum protection to conveyor belts while maintaining the efficiency of the conveyor systems.Features in Belt Cover:
- Advanced Polymer Technology: Gates uses advanced polymer materials in their belt covers, which offer excellent flexibility, strength, and resistance to chemicals. This allows the covers to adapt to different operating conditions.
- Enhanced Tensile Strength: The belt covers have high tensile strength, which means they can withstand heavy loads and prevent the belts from stretching or breaking.
- Good Sealing Performance: They provide a tight seal around the conveyor belts, preventing dust, dirt, and moisture from entering and damaging the belts.Advantages:
- Industry Experience: Gates has decades of experience in the power transmission industry, which gives them in - depth knowledge of the requirements of different applications.
- Quality Control: The company has strict quality control measures in place to ensure that every belt cover meets the highest standards of quality.
- Technical Support: Gates offers comprehensive technical support to its customers, helping them select the right belt cover for their specific needs.
4. Fenner Conveyors
Fenner Conveyors is a leading provider of conveyor belt solutions, including belt covers. The company has a strong presence in the mining, quarrying, and bulk handling industries.Fenner's belt covers are designed to withstand the harsh conditions of these industries, such as high - impact loads, abrasive materials, and extreme temperatures.Features in Belt Cover:
- Abrasion Resistance: Their belt covers are made from highly abrasion - resistant materials, which can extend the life of the conveyor belts in abrasive environments.
- Impact Resistance: Fenner's belt covers can absorb high - impact loads, protecting the belts from damage caused by falling rocks or other heavy objects.
- Fire - Retardant Options: In some industries, fire safety is a major concern. Fenner offers fire - retardant belt covers to meet the safety requirements of these applications.Advantages:
- Industry - Specific Solutions: Fenner understands the unique requirements of the mining and bulk handling industries and provides customized belt cover solutions for these sectors.
- Testing and Certification: The company conducts extensive testing on its belt covers to ensure they meet international standards and certifications.
- Long - Term Partnerships: Fenner has established long - term partnerships with many major mining and industrial companies, which is a testament to the quality of their products.
5. Bridgestone Corporation
Bridgestone Corporation is a well - known Japanese company famous for its tires and rubber products. It also offers a range of belt covers for industrial applications.Bridgestone's belt covers are developed with the company's advanced rubber technology. They are designed to provide reliable protection and performance in various industrial settings.Features in Belt Cover:
- Excellent Rubber Properties: The belt covers made by Bridgestone have excellent rubber properties, such as high elasticity, low rolling resistance, and good adhesion to the conveyor belts.
- Weather Resistance: They are resistant to weather conditions, including rain, snow, and sunlight, which makes them suitable for outdoor conveyor systems.
- Anti - Static Properties: In some industries, static electricity can be a problem. Bridgestone's belt covers can be designed with anti - static properties to prevent static build - up.Advantages:
- Research and Development: Bridgestone invests heavily in research and development to continuously improve the performance of its belt cover products.
- Global Manufacturing Network: The company has a global manufacturing network, which enables it to produce and supply belt covers efficiently to customers around the world.
- Environmental Considerations: Bridgestone is committed to environmental sustainability and develops belt covers that are more eco - friendly.
6. ContiTech AG
ContiTech AG, a division of Continental AG, specializes in rubber and plastic technology. It offers a variety of belt covers for different industrial applications.ContiTech's belt covers are characterized by their high - quality materials and precise manufacturing. They are designed to meet the strict requirements of industries such as food processing, pharmaceuticals, and electronics.Features in Belt Cover:
- Food - Grade Materials: In the food processing and pharmaceutical industries, hygiene is of utmost importance. ContiTech offers belt covers made from food - grade materials that comply with strict hygiene standards.
- Low - Friction Surface: The belt covers have a low - friction surface, which can reduce the energy consumption of the conveyor systems.
- Custom - Made Solutions: They can provide custom - made belt covers according to the specific needs of different industries, such as special shapes, sizes, and colors.Advantages:
- Quality Assurance: ContiTech has a rigorous quality assurance system in place to ensure the reliability and safety of its belt cover products.
- Technical Innovation: The company is at the forefront of technical innovation in the rubber and plastic industry, constantly introducing new features and improvements to its belt covers.
- Industry - Specific Knowledge: ContiTech has in - depth knowledge of the requirements of different industries, which allows them to provide tailored solutions.
7. Habasit AG
Habasit AG is a Swiss company that is a leading manufacturer of conveyor belts and belt covers. It has a global presence and serves a wide range of industries, including packaging, food processing, and logistics.Habasit's belt covers are known for their high - quality materials, precise manufacturing, and innovative designs.Features in Belt Cover:
- Modular Design: Habasit's belt covers have a modular design, which makes them easy to install, replace, and maintain. This can save time and costs for customers.
- Hygienic Design: In the food processing industry, Habasit's belt covers are designed to be hygienic, with smooth surfaces that are easy to clean and prevent the growth of bacteria.
- High - Speed Performance: Their belt covers can operate at high speeds, which is essential for industries that require fast - moving conveyor systems.Advantages:
- Customer - Centric Approach: Habasit focuses on understanding the needs of its customers and providing customized solutions to meet those needs.
- Training and Support: The company offers training and support to its customers, helping them optimize the performance of their conveyor systems with the right belt covers.
- Sustainable Solutions: Habasit is committed to developing sustainable belt cover products, using eco - friendly materials and manufacturing processes.
8. Forbo Siegling
Forbo Siegling is a leading provider of conveyor belts and belt covers in Europe. It has a strong presence in the industrial, food, and textile sectors.Forbo Siegling's belt covers are designed to meet the specific requirements of these industries, such as high - temperature resistance in the textile industry and hygiene in the food industry.Features in Belt Cover:
- Temperature Resistance: Their belt covers can withstand a wide range of temperatures, from low - temperature applications in cold storage to high - temperature applications in textile dyeing and finishing.
- Chemical Resistance: Forbo Siegling's belt covers are resistant to various chemicals, which makes them suitable for industries that use chemicals in their production processes.
- Anti - Microbial Properties: In the food industry, anti - microbial properties are important to prevent the growth of harmful bacteria. Forbo Siegling offers belt covers with anti - microbial treatments.Advantages:
- European Quality Standards: The company adheres to strict European quality standards, ensuring the high quality of its belt cover products.
- Local Support: With a network of local sales and service offices in Europe, Forbo Siegling can provide prompt and efficient support to its customers.
- Product Development: Forbo Siegling continuously invests in product development to meet the evolving needs of different industries.
9. Intralox
Intralox is a global leader in modular plastic conveyor belt systems and also offers belt covers. It is widely used in industries such as food processing, packaging, and automotive.Intralox's belt covers are designed to work seamlessly with their modular plastic conveyor belts, providing enhanced protection and performance.Features in Belt Cover:
- Compatibility: The belt covers are fully compatible with Intralox's modular plastic conveyor belts, ensuring a perfect fit and smooth operation.
- Easy Cleaning: They are easy to clean, which is important in industries where hygiene is a top priority, such as food processing.
- Customizable Configurations: Intralox can customize the belt covers according to the specific requirements of different conveyor systems, such as different widths and lengths.Advantages:
- System Integration: Intralox has expertise in integrating belt covers with their conveyor belt systems, which can optimize the overall performance of the conveyor systems.
- Continuous Improvement: The company is constantly improving its belt cover products based on customer feedback and technological advancements.
- Global Service Network: Intralox has a global service network that can provide quick response and support to customers around the world.
10. Sampla S.A.
Sampla S.A. is a Spanish company that specializes in conveyor belt solutions, including belt covers. It has a strong presence in the European market, particularly in the mining, cement, and steel industries.Sampla's belt covers are designed to withstand the harsh conditions of these industries, such as high - temperature, high - pressure, and abrasive environments.Features in Belt Cover:
- High - Temperature Resistance: Their belt covers can withstand extremely high temperatures, making them suitable for applications in steel mills and cement plants.
- Abrasion and Erosion Resistance: Sampla's belt covers are highly resistant to abrasion and erosion, which can extend the life of the conveyor belts in abrasive environments.
- Good Flexibility: They have good flexibility, which allows them to adapt to the movement of the conveyor belts without cracking or breaking.Advantages:
- Local Expertise: Sampla has in - depth knowledge of the European market and the specific requirements of local industries. This enables them to provide tailored solutions to their customers.
- Cost - Effective Solutions: They offer cost - effective belt cover products without compromising on quality, which is attractive to customers in cost - sensitive industries.
- Technical Support: Sampla provides comprehensive technical support to its customers, including on - site installation and maintenance services.
Summary
The top 10 belt cover suppliers in the world offer a wide range of products and services to meet the diverse needs of different industries. Each supplier has its own unique features and advantages. Hebei Juxin Conveyor Engineering Co., Ltd. stands out with its customization, high - quality materials, and competitive pricing. Continental AG, Gates Corporation, and other well - known companies bring their brand reputation, strong R & D capabilities, and global presence to the table. These suppliers play a crucial role in ensuring the smooth and efficient operation of conveyor systems around the world by providing reliable belt cover solutions. Whether it is protecting conveyor belts from harsh environmental conditions, enhancing safety, or improving the performance of the conveyor systems, these top suppliers are at the forefront of the industry, constantly innovating and improving their products to meet the evolving needs of their customers.